


Improving Consistency in Rear Lamp Production
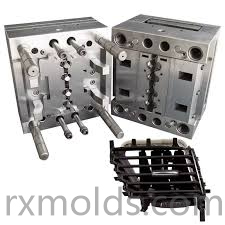
Rear lamp assemblies have become increasingly sophisticated as automotive manufacturers combine distinctive styling with functional lighting and compact component integration. A modern rear lamp may contain several molded parts, including outer lenses, inner optical elements, reflectors, decorative components, and structural housings. Each part must meet specific requirements for appearance, fit, and manufacturing consistency. Choosing a capable Rear Lamp Mold Manufacturer is therefore an important step in turning a lighting design into a practical production solution, particularly when the project involves complex surfaces and closely matched components.
The development process begins with understanding the product structure and its assembly relationships. Engineers review the component drawings and three-dimensional models to identify critical dimensions, visible surfaces, fastening points, and interfaces with adjacent parts. A lens may require precise optical contours, while a housing may need stable mounting features and sufficient mechanical strength. Parting lines should be positioned to minimize their influence on visible areas. Undercuts, side openings, and complicated contours must also be identified because they may require additional mold mechanisms. Early technical communication helps ensure that tooling decisions match the customer's actual design and production expectations.
Material selection should reflect the performance requirements of each component. Transparent lenses may use polycarbonate or acrylic, depending on the desired combination of optical clarity, impact resistance, and environmental durability. Housings and internal supports may use other thermoplastics chosen for stiffness, thermal properties, and dimensional stability. Material shrinkage affects cavity dimensions, while melt viscosity influences filling and gate design. Some materials may require controlled drying or specific processing conditions. Understanding these characteristics allows engineers to develop a mold that is compatible with the selected resin rather than relying on general assumptions.
Surface engineering is particularly important for visible rear lamp components. The cavity must reproduce the intended contours and finish while limiting marks that could affect the final appearance. Precision machining establishes the geometry, and polishing can provide the required optical or decorative surface. Textured regions may require different finishing methods depending on the design. Inspection should verify not only the overall surface but also transitions, edges, and detailed features. Because polished surfaces can be easily damaged, protective handling and appropriate cleaning procedures should be incorporated into the manufacturing process.
The filling system determines how molten material enters and moves through the cavity. Gate location can influence flow direction, weld-line positions, filling balance, and pressure requirements. If the component has thin walls or long flow paths, filling may become difficult. Air trapped near the end of a flow path can produce burn marks or incomplete details when venting is inadequate. Mold flow analysis can help evaluate these risks before mold construction is completed. By comparing possible gate and runner arrangements, engineers can make informed adjustments that support more consistent cavity filling.
Cooling-system design is another major factor in dimensional control. Rear lamp components may combine large surfaces with thicker mounting sections, ribs, or structural features. Different areas can retain heat for different periods, resulting in uneven shrinkage if cooling is not properly balanced. Cooling channels should be arranged to remove heat efficiently while preserving mold strength and allowing practical maintenance. The design must also consider the expected production cycle and the material's cooling behavior. Effective thermal management supports stable dimensions and reduces the likelihood of warpage after ejection.
Mold construction requires accuracy across both stationary and moving components. CNC machining produces cavity profiles and fitting interfaces, while EDM supports detailed features that are difficult to machine conventionally. Core and cavity inserts must align correctly, and guide systems should maintain smooth movement throughout repeated cycles. Slides and lifters may be required to release undercuts, while ejector pins and sleeves must remove parts without damaging cosmetic surfaces. Inspection during machining and assembly helps verify critical dimensions before the tool proceeds to trial production.
Trial molding allows the engineering team to evaluate the complete system under practical conditions. Initial samples are checked for dimensions, surface appearance, filling quality, demolding, and assembly compatibility. Processing parameters such as injection speed, holding pressure, melt temperature, and cooling time are adjusted according to the material and part design. Defects should be investigated systematically. For example, warpage may be connected to cooling imbalance or uneven wall thickness, while visible flow marks may relate to gate position or processing conditions. Trial documentation helps establish a repeatable production window and provides a reference for future adjustments.
Long-term performance depends on preventive maintenance and clear quality procedures. Mold surfaces should be cleaned and inspected regularly, particularly in optical areas. Vents, cooling channels, slides, and ejector mechanisms also require routine attention. Wear or contamination can gradually affect surface appearance and dimensional consistency, even when the initial mold performs well. Manufacturers should retain maintenance histories and inspection results to support traceability and planned servicing. Clear communication about drawing revisions, resin grades, and acceptance criteria is also important for automotive supply programs.
A tooling partner should provide engineering support throughout design review, mold manufacturing, trial validation, and production preparation. Taizhou Renxin Mould Co., Ltd. works with customers on automotive mold projects requiring coordinated engineering and manufacturing. Buyers can visit https://www.rxmolds.com to discuss component geometry, material selection, optical requirements, and tooling plans when evaluating a Rear Lamp Mold Manufacturer for a new automotive lighting program.

 English
 Arabic
 Spanish
 Portuguese
 Deutsch
 Turkish
 Dutch
 Italiano
 Russian
 Romaian
 Portuguese (Brazil)
 Greek